为什么食品工厂需要在输送线上安装金属探测器 - 如果跳过它们会发生什么
我有一次看到俄亥俄州一家中型面包店的生产经理从密封的餐卷袋中拉出一个微小的螺丝碎片——在有人通过塑料发现闪光之前,它已经跑了三遍传送带了。. 该线路已运行了六个小时. 算一下在此之前有多少包被扔掉了.
这是食品安全研讨会上没人谈论的事情: 金属污染不会自行显现. 破损的搅拌机叶片不会戏剧性地脱落. 它会脱落微碎片. 磨损的传送带紧固件失去了 2 毫米的夹子. 架空管道螺钉在数周内振动松动, 不是秒.
每一件作品最终都会出现在您的产品中.
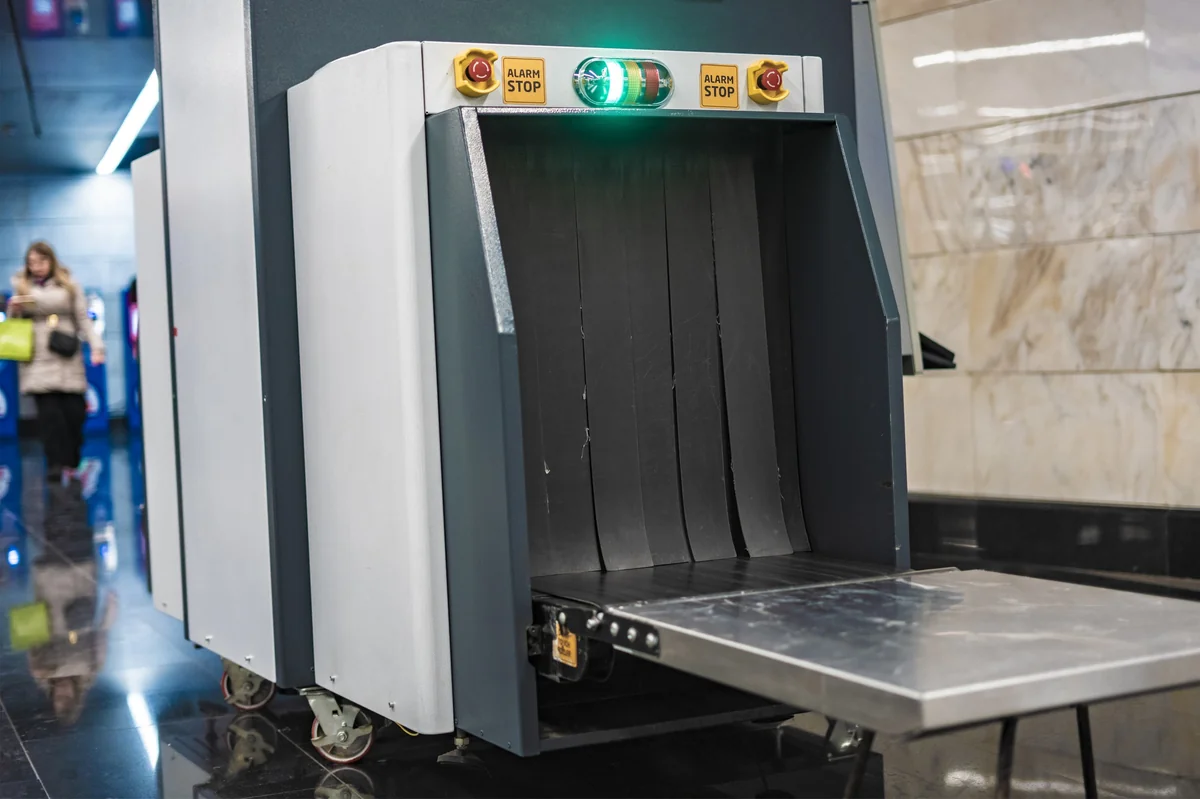
一个 传送带金属探测器 位于最重要的位置——运动点, 当产品已经包装或即将包装时. 并不光鲜亮丽. 但这是托盘运送到供货经销商之前的最后一个可靠检查站 47 横跨两个州的杂货店. 错过那里的污染物, 而且你不记得一批. 您正在回想起该轮班期间发生的所有事情, 也许那一整天.
财务打击比大多数工厂经理公开承认的还要严重. 典型的金属污染召回(即使没有人受伤)发生在 $400,000 和 $2.1 考虑处置成本时为 100 万, 客户通知, and the FDA paperwork avalanche (哪个, 诚实地, is its own special kind of hell). That’s before you account for the brand damage. Consumers forgive a lot of things. Finding a metal shard in their kid’s cereal is not one of them.
So what happens if you skip the detector entirely? Some smaller operations do — they rely on manual checks or upstream equipment and hope for the best. Works fine until it doesn’t. Then you’re either paying for the recall or, worse, waiting for the lawsuit after someone chips a tooth on a staple fragment that made it into a granola bar.
Not a risk I’d take. But I’ve seen people try.
How to Choose the Right Conveyor Belt Metal Detector for Your Food Processing Line
I spent about an hour last week on the phone with a bakery owner in Ohio who bought the wrong detector. Not defective — just wrong for what he needed. He’d gone with the cheapest unit he could find online, figured metal detection was metal detection, and now he’s got a machine that false-triggers every time a loaf pan with a slight aluminum residue passes through. Cost him $8,200. Basically a very expensive paperweight.
Don’t be that guy.
First thing: match the aperture size to your actual conveyor width. 听起来很明显, but people screw this up constantly. You need at least 2-3 inches of clearance on each side of your product flow — detectors work best when the product stays centered in the detection zone. I’ve seen operations try to cram 18-inch-wide trays through a 20-inch aperture and wonder why they’re getting inconsistent reads.
Sensitivity is where it gets tricky. You want a conveyor belt metal detector that can catch ferrous particles down to 1.5mm, non-ferrous around 2.0mm, and stainless steel fragments at 2.5mm or better — those are the HACCP benchmarks most auditors expect in 2026. But (and this matters) higher sensitivity means more false rejects if your environment is noisy. Magnetic interference from nearby motors, vibration from older conveyors, even the metal fasteners in your belt itself can throw off cheaper units.
Here’s what actually matters when you’re comparing models:
| Feature | Why It Matters | Don’t Cheap Out If… |
|---|---|---|
| Multi-frequency scanning | Reduces false positives from product effect (wet, salty, or conductive foods) | You run anything with high moisture or salt content |
| Auto-reject mechanism | Physically removes contaminated product without stopping the line | You’re processing more than 50 units/minute |
| IP69K rating | Survives high-pressure washdowns in wet production environments | You clean lines daily with spray systems |
| Data logging & connectivity | Tracks every reject event for audit trails and trend analysis | You’re SQF or BRC certified (or trying to be) |
And honestly? Talk to your packaging team before you buy. The reject bin needs to integrate with your existing conveyor setup, and I’ve watched installations go sideways because nobody measured the vertical clearance for a pneumatic pusher arm. Small detail. Expensive fix.
Installation and Integration: Making Metal Detection Work With Your Existing Conveyor System
OK so here’s where most installations either go smoothly or turn into a three-week nightmare — and the difference usually comes down to whether you measured twice before ordering.
First thing: conveyor speed matters more than people think. Your metal detector needs a minimum “dwell time” for each product to pass through the aperture. If you’re running a high-speed line at 120 feet per minute, you can’t just bolt on a detector designed for 60 FPM and expect it to catch everything. I watched a bakery do exactly this in 2026 — they were getting false negatives on small ferrous fragments because products were zipping through too fast for the detection coil to register them. Had to swap the entire head unit. Not cheap.
Height clearance is the other gotcha. Measure from your belt surface to any overhead structures — then add at least 8 inches for the detector frame itself, plus whatever your reject mechanism needs. Pneumatic pushers need vertical space. Air blasts need less, but they’re not great for heavy products.
And here’s something nobody tells you upfront: your existing conveyor frame might need reinforcement. Metal detectors are heavier than they look (we’re talking 150-300 pounds depending on aperture size), and vibration from the conveyor motor can throw off calibration if the mounting isn’t rigid. I’ve seen facilities weld in cross-bracing after installation because the detector kept auto-rejecting good product due to mechanical noise.
The actual integration sequence usually goes like this:
- Stop signal wiring — detector talks to your conveyor PLC to pause the line during rejects
- Reject mechanism sync — pusher arm or air blast fires at exactly the right moment
- Upstream sensor tie-in — so the detector knows when a product is entering the aperture
- Data output connection — if you’re logging to a central SCADA system or cloud platform
Most modern units use Ethernet IP or Modbus RTU for this stuff, but I still run into older conveyors with relay-based controls. You can make it work — you just need the right interface module (and maybe an electrician who remembers how to wire 24VDC circuits).
One last thing. Test your reject bin capacity before you go live. If your line produces 200 units per hour and your false reject rate is even 2%, that’s four units per hour going into the bin. Sounds manageable until second shift forgets to empty it and you’ve got product piling up at 2 AM.
Sensitivity Settings, Rejection Systems, and Keeping Your Metal Detector Actually Working
So here’s the thing nobody tells you until you’ve already spent the money: sensitivity isn’t a “set it and forget it” dial. I learned this the hard way on a snack line in 2026 when we kept getting false rejects on foil-wrapped granola bars. Cranked the sensitivity down to stop the nuisance alarms, and two weeks later a stainless steel washer made it through because we’d basically turned the detector into a very expensive tunnel.
You need to calibrate for your actual product. Not the theoretical spec sheet product — the real stuff coming down your line with all its moisture content variations and temperature swings and packaging inconsistencies.
Most conveyor belt metal detectors let you save multiple product profiles (my current Mettler-Toledo unit holds 200). Use them. Different sensitivities for different SKUs. Your dry pasta needs way less aggressive settings than your canned tomatoes, because the product effect is totally different.
And test your reject system every single shift. Not once a week. Every shift.
I use ferrous, 有色金属, and stainless test pieces — the little metal spheres that come with the detector — and I run them through at the start of every production run. Takes ninety seconds. The reject arm should activate, the product should divert into the bin, and you should get a logged event in your HMI. If any part of that chain fails, you’ve got a compliance problem waiting to happen.
Here’s what actually breaks on these systems:
- Photoelectric sensors get dirty (especially in dusty environments like flour mills)
- Reject arms lose air pressure — check your pneumatic lines monthly
- Solenoid valves stick after a few thousand cycles
- Conveyor belts stretch over time, which throws off your sensor timing
Keep a maintenance log. Seriously. When the health inspector shows up, “we test it regularly” doesn’t cut it anymore — you need timestamped records showing that you ran test pieces and documented the results. Most modern detectors will generate this automatically if you’ve got them networked, but if you’re running an older standalone unit, you’re doing it manually in a logbook.
One more thing that’ll save you a service call: clean the aperture every week with a non-metallic brush. Product buildup changes the electromagnetic field characteristics, which gradually shifts your baseline and increases false rejects.
结论
所以这是交易: a conveyor belt metal detector only works if you actually maintain it. I’ve seen too many operations drop $15K on a system, run it hard for six months, then wonder why they’re getting phantom rejects or — way worse — missing actual contamination. Clean that aperture weekly. Run your test pieces daily. Keep the logbook current.
And honestly? If your reject mechanism is acting weird, start with the pneumatics before you call service. Nine times out of ten it’s a $4 air fitting that’s gone bad, not the $800 control board.
Your detector is only as good as the person running it. Train your line operators properly, and they’ll catch problems before they become recalls.
常见问题解答
问: How much does a conveyor belt metal detector actually cost?
一个: Entry-level units start around $8K for basic ferrous detection on slow lines. Mid-range systems with full ferrous/non-ferrous/stainless capability run $12K-$18K, and if you need multi-frequency detection for wet products or pharmaceutical-grade sensitivity, you’re looking at $25K+. Installation and integration usually add another 15-20% on top.
问: What’s the difference between ferrous and non-ferrous detection?
一个: Ferrous metals (steel, iron) are magnetic and way easier to detect — your conveyor belt metal detector will catch a 2mm steel fragment no problem. Non-ferrous metals like aluminum, brass, or copper don’t have magnetic properties, so they require higher sensitivity settings and better coil design. Stainless steel is the nightmare scenario because it’s weakly magnetic and requires the most sensitive (and expensive) detection systems.
问: Can a metal detector work on an existing conveyor belt?
一个: 绝对地, but your belt better not have metal fasteners or reinforcement cables running through it. Most retrofit installations use tunnel-style detectors that mount around the existing frame — just make sure you’ve got at least 12 inches of clear belt on either side of the aperture for the magnetic field to stabilize.
问: How often do you need to calibrate a conveyor belt metal detector?
一个: Daily test piece verification is non-negotiable if you’re running food production. Full recalibration depends on your product — if you’re running the same SKU all day, maybe monthly. But if you switch between wet and dry products or change pack sizes, recalibrate every changeover. Temperature swings and vibration will drift your settings faster than you think.
问: Why does my metal detector reject good product?
一个: Nine times out of ten it’s product effect — moisture, salt content, or temperature variations are throwing off the phase signal. The other culprit is a dirty aperture where product buildup is creating interference. Start by running your test pieces to verify actual sensitivity, then check for environmental factors like a forklift driving past or a motor kicking on nearby.
问: What size metal fragment can these detectors actually catch?
一个: On a properly tuned conveyor belt metal detector running dry product, you should catch 1.5mm ferrous, 2.0mm non-ferrous, and 2.5mm stainless as a baseline. Wet or conductive products (like fresh meat or cheese) cut that sensitivity in half — maybe worse. Anyone promising sub-1mm detection on high-moisture product is either lying or selling you a $40K pharmaceutical-grade system.
问: Do metal detectors slow down production lines?
一个: Not if you size them right. Most industrial units handle belt speeds up to 400 feet per minute without breaking a sweat. The reject mechanism is usually your bottleneck — pneumatic pushers need about 0.3 seconds to actuate, so at high speeds you need proper spacing between products or you’ll reject clean ones along with the contaminated.